


In appliance showrooms, a refrigerator door or oven handle has only seconds to communicate quality. Before buyers compare compressors, smart controls, or energy ratings, they judge how the surface reflects light, resists fingerprints, and feels under the hand. For manufacturers, surface finishing is not cosmetic afterthought work; it is a measurable driver of perceived value, defect rates, cleaning performance, and retail pricing power. This article examines the finishing choices that shape modern kitchen appliances, from brushed stainless steel and mirror polishing to powder coating, PVD, anodizing, and anti-fingerprint treatments. It also explains the technical standards—such as gloss consistency, abrasive grit, and Ra roughness—that help brands turn durable surfaces into market differentiation.
Why Surface Finishing Shapes Kitchen Appliance Brand Value
Kitchen appliance surface finishing represents a critical intersection of engineering and design. While internal components dictate functionality, the exterior finish is the primary interface between the product and the consumer. Strategically, surface treatments account for a significant portion of total unit manufacturing costs, yet they disproportionately drive market positioning and retail pricing power.
How finishes influence first impressions and perceived quality
The showroom environment heavily relies on immediate visual impact. When consumers evaluate premium appliances, their first impression is dictated by how light interacts with the surface. A flawless, uniform finish signals precision engineering and high manufacturing standards, whereas inconsistent texturing or uneven gloss levels immediately degrade perceived quality. Consequently, brands leverage bespoke finishes to differentiate themselves in saturated retail spaces, transforming standard utility items into highly differentiated products.
Key visual and tactile attributes buyers notice
Buyers subconsciously evaluate appliances through both visual and tactile feedback. Visually, color consistency and gloss levels are paramount; a variance of more than a few gloss units between a refrigerator door and its adjacent handle is readily noticeable and often interpreted as a manufacturing defect. Tactilely, surface roughness—measured in Ra (average roughness)—plays a crucial role. High-end smooth finishes typically require an Ra value of less than 0.4 µm, ensuring the appliance feels premium to the touch while simultaneously resisting the accumulation of daily dirt and oils.
Essential surface finishing terms manufacturers should define
To maintain consistency across global supply chains, manufacturers must standardize their finishing terminology. Key terms include Physical Vapor Deposition (PVD), a high-vacuum coating process that bonds metallic layers at the atomic level for extreme durability; anodizing, an electrochemical process that thickens the natural oxide layer on aluminum parts; and powder coating, a dry finishing process cured under heat to form a protective skin. Precise definitions of these processes prevent miscommunication with outsourced vendors and significantly reduce defect rates during mass production.
Kitchen Appliance Surface Finishing Options Compared
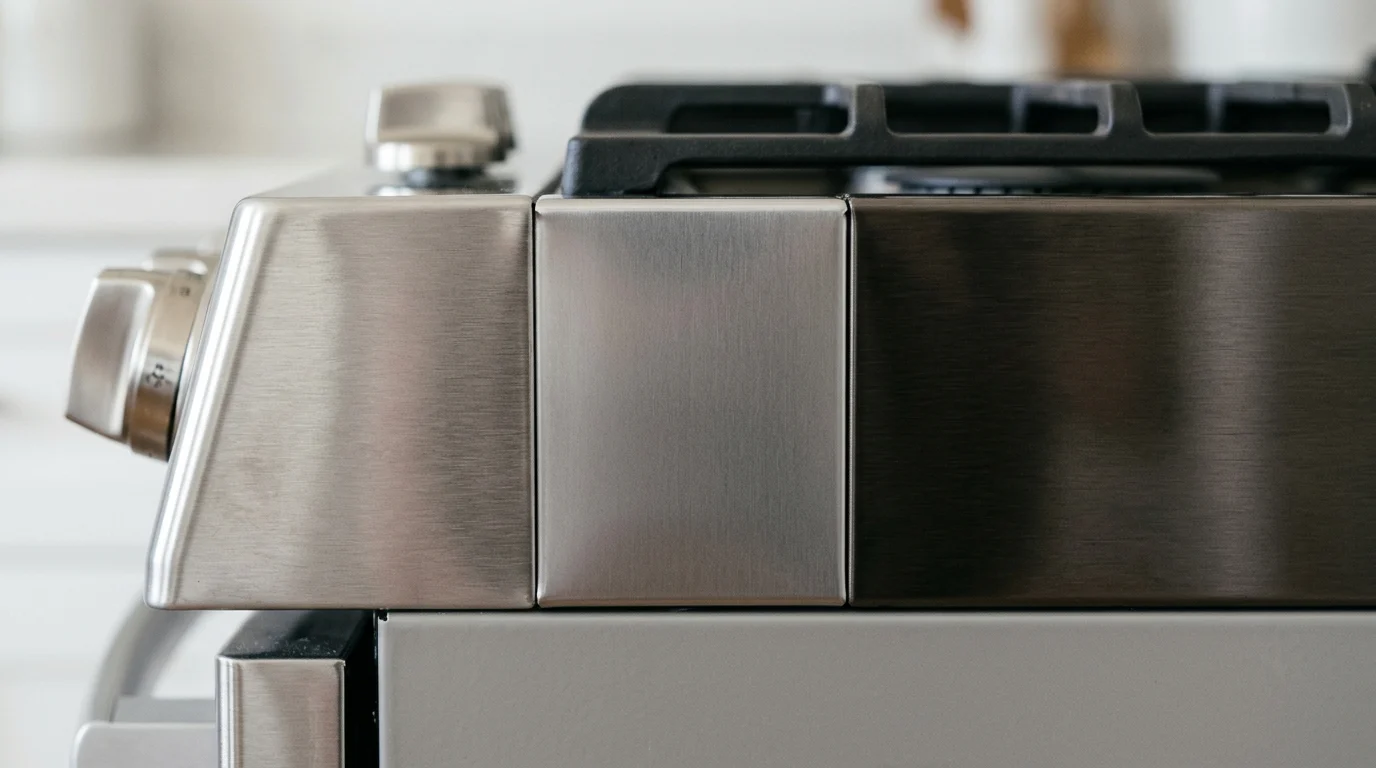
The landscape of kitchen appliance surface finishing encompasses a broad spectrum of mechanical and chemical treatments. Selecting the appropriate option requires balancing aesthetic desires with rigorous daily durability requirements.
Brushed, polished, coated, and anti-fingerprint finishes
The industry standard for stainless steel remains the No. 4 brushed finish, characterized by short, parallel polishing lines typically achieved using 120- to 150-grit abrasives. Polished or No. 8 mirror finishes offer high reflectivity but demand immaculate upkeep, limiting their use to low-touch accents. Coated finishes, particularly powder coats, introduce vibrant color palettes and matte textures to the kitchen environment. In premium and mid-tier segments, Anti-Fingerprint (AFP) treatments have transitioned from a luxury feature to a common expectation. While advanced versions utilize oleophobic nano-coatings to repel oils, simpler polymer-based clear coats are also used to reduce smudging on high-traffic touchpoints.
Scratch resistance, cleanability, durability, and cost
Manufacturers must evaluate finishes against daily operational hazards. A comprehensive assessment includes scratch resistance, cleanability, overall lifecycle durability, and the cost per square meter to apply the treatment.
| Finish Type | Scratch Resistance | Cleanability | Relative Cost Multiplier | Typical Application |
|---|---|---|---|---|
| No. 4 Brushed | Moderate | High | 1.0x (Baseline) | Standard Ovens, Fridges |
| Powder Coated | High | Moderate | 1.2x | Stand Mixers, Kettles |
| AFP Stainless | Moderate | Very High | 1.5x | Premium Refrigerators |
| PVD Coating | Very High | High | 2.5x | Luxury Ranges, Hardware |
When to use premium finishes for higher-end appliances
Premium finishes are deployed strategically to justify higher price points in the luxury appliance segment. For instance, advanced PVD coatings can cost up to 2.5 times more than standard stainless steel finishing—though pricing is heavily volume-dependent—but they enable highly sought-after aesthetics like matte black, brushed brass, or rose gold. These advanced finishes are exceptionally resistant to tarnishing and wear, making them ideal for flagship product lines where the consumer is willing to pay a premium for exclusivity and advanced design integration.
Materials, Process Control, and Quality Testing
Achieving a flawless finish is not solely dependent on the coating material; it requires a holistic approach encompassing substrate selection, stringent process controls, and rigorous quality assurance testing.
How substrate choice affects final finish quality
The underlying substrate dictates the ultimate quality and longevity of the finish. For example, austenitic 304 stainless steel, containing 18% chromium and 8% nickel, provides a superior, corrosion-resistant base for brushing and coating compared to the more economical ferritic 430 stainless steel. Beyond stainless, modern appliances frequently utilize cold-rolled steel with enamel coatings for oven cavities, aluminum die-castings for stand mixer housings, and engineering plastics for consumer-facing touchpoints. Regardless of the material, if the chosen substrate contains micro-porosities, uneven grain structures, or surface impurities, even the most advanced chemical coatings will fail prematurely through blistering or delamination.
Critical process controls from preparation to curing
Process control during application is critical to minimizing batch defect rates. Surface preparation often involves multi-stage alkaline degreasing and ultrasonic cleaning to completely remove machining oils and particulate matter. During the application phase, environmental controls are mandatory; powder coating lines, for instance, must maintain strict ambient humidity levels and utilize curing ovens tightly calibrated to specific temperatures and durations—which vary significantly depending on the specific resin chemistry—to achieve the proper cross-linking of the polymers.
Quality tests for adhesion, corrosion, wear, and appearance
Finished components must undergo standardized testing to validate their performance against international benchmarks established by organizations like ISO. Skipping these protocols exposes manufacturers to high warranty claims.
| Quality Test | Standard Reference | Target Metric | Purpose |
|---|---|---|---|
| Salt Spray Test | ASTM B117 / ISO 9227 | > 500 hours | Evaluates long-term corrosion resistance |
| Cross-Hatch Adhesion | ASTM D3359 | 5B (0% peeling) | Measures coating bond strength to substrate |
| Pencil Hardness | ASTM D3363 | 2H to 4H | Determines baseline scratch resistance |
| Gloss Measurement | ASTM D523 | +/- 5 Gloss Units | Ensures visual consistency across batches |
Compliance, Sourcing, and Handling Considerations
Beyond aesthetics and durability, kitchen appliance surface finishing must navigate a complex web of regulatory compliance, strategic sourcing decisions, and logistical handling protocols to ensure products reach the consumer intact.
Food-contact, chemical, and environmental requirements
Finishes applied to kitchen appliances face strict regulatory scrutiny, particularly concerning food-contact safety and environmental impact. Coatings used on internal oven cavities, mixer attachments, or interior bins must comply with FDA guidelines or equivalent international standards, ensuring no toxic leaching occurs under high heat or acidic conditions. Furthermore, global environmental directives like RoHS and REACH mandate strict thresholds for hazardous substances, requiring that heavy metals such as hexavalent chromium or lead be kept strictly below 0.1% by weight in any finishing compound.
In-house finishing versus outsourced finishing partners
Manufacturers must decide whether to invest heavily in in-house finishing lines or utilize specialized outsourced partners. In-house lines require substantial capital expenditure for automated powder coating or electroplating facilities, but offer total process control. Outsourcing shifts the capital burden but introduces Minimum Order Quantities (MOQs) and requires robust vendor auditing. Global supply chain flow data from TradeMap highlights the extensive cross-border movement of pre-finished appliance panels, underscoring the importance of reliable sourcing partnerships.
Packaging, storage, and transport risks that damage finishes
A premium finish is useless if it is damaged before final installation. Packaging and transport pose significant risks to surface integrity. To mitigate abrasion and chemical etching during transit, finished panels are typically protected with specialized Polyethylene (PE) films. Storage environments must also be climate-controlled; excessive heat or prolonged UV exposure in warehouses can cause protective film adhesives to bake into the appliance surface, resulting in permanent ghosting or staining upon removal.
How Manufacturers Should Choose the Right Finish
Finalizing the surface finishing strategy is a cross-functional endeavor that directly impacts market viability, production costs, and overall brand perception.
Matching finish selection to product positioning
Finish selection must align directly with the appliance's market positioning. Mass-market products require high-yield, cost-effective finishes like standard powder coats or basic brushed stainless steel, where profit margins are tight and production volumes are high. Conversely, professional-grade or luxury appliances demand specialized treatments like AFP coatings or custom PVD colors, aligning the physical product with the target demographic and justifying the higher retail price.
Writing clear and measurable finish specifications
Vague aesthetic descriptions inevitably lead to supply chain disputes and inconsistent product runs. Manufacturers must write objective, measurable finish specifications. Instead of requesting a "shiny black finish," engineering documents should specify a target, such as 85 Gloss Units (GU) measured at a 60-degree angle, with a strict tolerance of +/- 5 GU. Acceptable Quality Limits (AQL) must also be defined, such as an AQL of 1.5 for major visual defects, ensuring vendors have clear, quantifiable targets.
Aligning design, engineering, quality, and procurement teams
Successful execution requires seamless alignment between design, engineering, quality assurance, and procurement teams. Designers may push for a novel matte texture to follow a trend, but engineering must validate its cleanability, and procurement must evaluate the potential per-unit cost increase. By establishing a collaborative framework early in the product development lifecycle, manufacturers can optimize kitchen appliance surface finishing to deliver reliable products while maintaining rigorous quality and cost controls.
Key Takeaways
- Define finish specifications early, including gloss level, color tolerance, grit, Ra, and coating type, to prevent visible mismatch between panels, handles, and trim.
- Use an Ra target below 0.4 µm for premium smooth surfaces where tactile feel, cleanability, and oil resistance are major purchase drivers.
- Specify No. 4 brushed stainless steel with 120- to 150-grit abrasive patterns when the goal is a durable, familiar appliance finish.
- Evaluate every finish by scratch resistance, cleanability, lifecycle durability, and cost per square meter rather than appearance alone.
- Treat anti-fingerprint coatings as a mainstream requirement for mid-tier and premium appliances, especially on doors, handles, and control areas.
- Standardize process terminology such as PVD, anodizing, powder coating, and AFP across suppliers to reduce defect rates during scale production.
Frequently Asked Questions
Why does surface finishing affect appliance brand value?
The finish is the first feature buyers see and touch. Uniform gloss, color, texture, and feel signal manufacturing precision, helping brands justify premium positioning and reduce the perception of defects.
What Ra value is typical for a premium smooth appliance finish?
High-end smooth finishes often target an Ra value below 0.4 µm. This improves tactile quality while helping surfaces resist dirt, oil, and daily residue buildup.
What is a No. 4 brushed stainless steel finish?
A No. 4 finish is a common appliance-grade brushed surface with short, parallel polishing lines, typically produced using 120- to 150-grit abrasives.
Are anti-fingerprint finishes now standard in kitchen appliances?
In many mid-tier and premium appliances, anti-fingerprint treatments are now expected. They reduce smudging on high-touch areas through polymer clear coats or oleophobic nano-coatings.
How can manufacturers reduce surface finish defects across suppliers?
They should standardize terms such as PVD, anodizing, powder coating, gloss level, grit, and Ra. Clear specifications reduce vendor misinterpretation and improve consistency in mass production.