


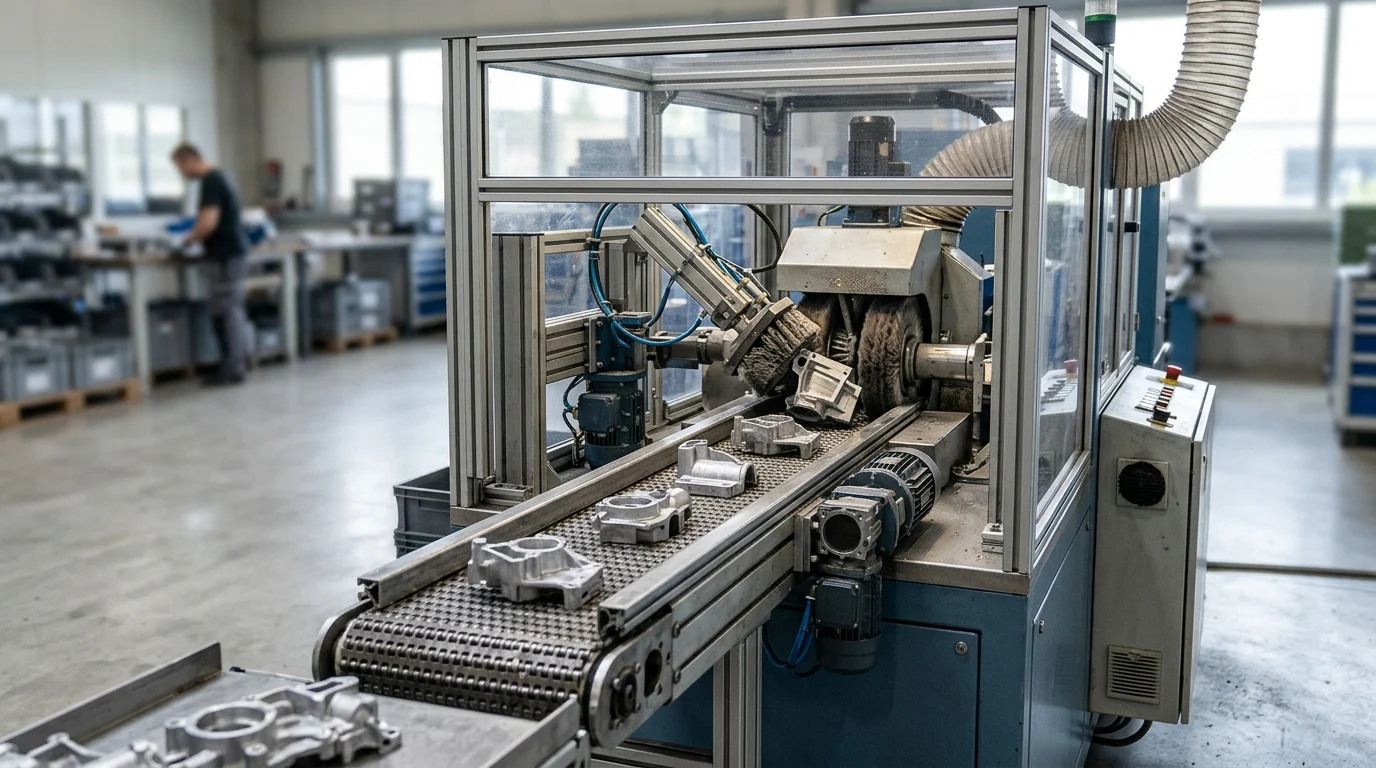
In high-volume metal fabrication, deburring is often the hidden constraint between cutting and value-added operations such as bending, welding, and coating. A conveyor-based deburring system turns that constraint into a continuous, measurable process by moving parts under controlled abrasive stations at adjustable feed rates. Instead of relying on manual touch, operator judgment, or batch queues, manufacturers can achieve repeatable edge rounding, safer handling, and faster downstream flow. This article explains how conveyor deburring cells work, where they outperform manual grinding and tumbling, and which technical factors—such as working width, feed speed, and edge consistency—matter most when evaluating an automated finishing investment.
Why Choose a Linear Conveyor Deburring Cell
Industrial metal fabrication increasingly relies on automated surface finishing to maintain profit margins and meet strict quality standards. A linear conveyor deburring cell stands out as a high-throughput solution that seamlessly integrates into modern production lines. By moving flat or semi-flat parts continuously under a series of abrasive heads, this equipment eliminates the bottlenecks associated with manual grinding and batch processing.
What Defines a Conveyor Deburring Cell
A conveyor deburring cell is defined by its continuous feed mechanism, typically utilizing an endless high-friction belt or a series of pinch rollers to transport sheet metal, machined plates, or extrusions through a processing zone. Standard working widths range from 600mm for compact operations up to 1500mm or more for large-format laser-cut sheets. The cell houses multiple processing stations—such as wide abrasive belts, rotary brushes, or oscillating discs—housed within a single enclosed chassis.
How Linear Conveyors Support Continuous Production
Unlike batch systems, linear conveyors support one-piece flow, allowing parts to transition directly from upstream cutting processes into the finishing stage. Feed rates are typically adjustable via variable frequency drives (VFDs), operating anywhere from 1.0 to 10.0 meters per minute depending on the severity of the burr and the desired edge radius. This continuous motion ensures that downstream operations, such as bending, welding, or coating, are constantly fed with clean, safe-to-handle components, effectively eliminating work-in-progress (WIP) inventory buildup.
How to Compare Conveyor Deburring with Other Methods
Selecting the optimal finishing technology requires a careful evaluation of how different methods balance speed, quality, and operational costs. While some shops default to manual grinding out of habit, scaling production inevitably exposes the limitations of human labor in both consistency and throughput.
Key Throughput and Quality Comparison Points
When comparing deburring methods, throughput and surface quality are the primary metrics. A conveyor deburring cell can process hundreds of parts per hour, maintaining strict tolerances on edge rounding—often achieving a uniform radius of up to 2.0mm across all part edges simultaneously. Furthermore, automated cells conform strictly to international standards, such as those published by the ISO for surface roughness and edge conditions, ensuring that every part meets exact engineering specifications without operator-to-operator variance.
Manual Deburring vs Batch Tumbling vs Conveyor Deburring
To illustrate the operational differences, the table below compares three common approaches to metal finishing across critical production variables.
| Finishing Method | Throughput | Labor Dependency | Edge Consistency | Max Part Size Handling |
|---|---|---|---|---|
| Manual Deburring | Low (5-20 parts/hr) | Very High (1 operator per station) | Highly Variable | Limited by manual lifting |
| Batch Tumbling | Medium (Batch dependent) | Low (Loading/unloading only) | Good, but non-selective | Small to Medium (<300mm) |
| Conveyor Deburring | Very High (Continuous) | Low (Feeding/catching) | Highly Consistent | Large (Up to 1500mm wide) |
Batch tumbling is cost-effective for small components but cannot handle large, flat sheets without causing part-on-part impingement. Manual deburring is flexible but suffers from high ergonomic risks and inconsistent quality. The conveyor deburring cell bridges these gaps by offering high-speed, repeatable processing for a wide range of part sizes.
Key Specifications That Determine Performance
The performance of a linear conveyor deburring cell is dictated by its internal configuration and the specific technologies utilized to remove material. Understanding these specifications is critical for matching the machine to the specific alloys, thicknesses, and burr profiles present in a facility.
Conveyor Speed, Abrasive Media, and Brush Configuration
The core of the cell's performance lies in the combination of conveyor speed, abrasive media, and brush configuration. Machines are typically equipped with two to four heads. A primary wide belt head aggressively removes vertical dross and heavy burrs, while secondary cross belts or rotary brushes soften the edges. The table below outlines typical tool configurations and their expected lifecycles.
| Abrasive Configuration | Primary Function | Typical Tool Life (Operating Hours) |
|---|---|---|
| Wide Abrasive Belt | Heavy burr and slag removal | 40 - 80 |
| Rotary Brushes (Wire/Nylon) | Uniform edge rounding and oxide removal | 300 - 500 |
| Oscillating Discs | Multi-directional surface finishing | 200 - 400 |
Operators must balance the conveyor speed (typically 0.5 to 8.0 m/min) with the rotational speed of the brushes to optimize both finish quality and consumable longevity.
Edge Radius and Surface Finish Inspection Criteria
Precision manufacturing often requires specific inspection criteria for edge radius and surface finish. For aerospace and medical components, a conveyor deburring cell must consistently achieve a Roughness average (Ra) of less than 0.8 micrometers. Modern cells incorporate digital thickness adjustments with a precision of 0.01mm, allowing the abrasive heads to apply exact pressure to the material surface, ensuring that the critical dimensions of the part are not altered during the deburring process.
Dust Extraction, Coolant Management, and Guarding
Material removal generates significant byproducts, necessitating robust extraction and coolant management systems. Dry deburring cells require high-capacity dust extraction units pulling a minimum of 1500 CFM to safely evacuate combustible particulate, especially when processing aluminum or titanium. Alternatively, wet deburring systems utilize flood coolant to suppress dust and dissipate heat, requiring integrated paper bed filters (typically 50-micron mesh) to separate metal swarf from the recirculating fluid. Proper guarding and interlocks are standard to protect operators from pinch points and airborne debris.
How to Implement a Linear Conveyor Deburring Cell
Deploying a new automated finishing system requires more than simply dropping the machine onto the shop floor. A systematic implementation strategy ensures that the equipment achieves its intended return on investment without disrupting existing production schedules.
Map Part Families and Burr Conditions
The first step in implementation is mapping part families and assessing existing burr conditions. Facility managers should categorize parts by material type, thickness (e.g., standardizing batches within a 1mm to 50mm thickness range), and the severity of the burr generated by upstream cutting lasers or punches. Grouping parts with similar finishing requirements minimizes the need for operators to constantly adjust machine parameters or swap out abrasive media, thereby maximizing continuous run time.
Validate Cycle Time, Tool Wear, and Quality
Before full-scale production begins, it is essential to validate cycle times, tool wear, and part quality through rigorous sample testing. Manufacturers should run test batches to establish baseline data for abrasive degradation and processing speed. The goal is to calibrate the system to achieve an Overall Equipment Effectiveness (OEE) of 85% or higher, a standard metric detailed extensively in industrial engineering literature (such as resources found via Wikipedia under manufacturing metrics). Validating these parameters prevents bottlenecks and ensures the cell meets daily throughput quotas.
Plan Maintenance and Consumable Replacement
Continuous production relies on proactive maintenance and a well-planned consumable replacement schedule. A linear conveyor deburring cell requires regular checks on conveyor belt tracking, bearing lubrication, and abrasive wear. Facilities should plan for routine downtime; for instance, a complete changeover of rotary brushes typically takes 15 to 30 minutes. By scheduling these maintenance windows during shift changes or planned outages, operators can prevent catastrophic tooling failures and maintain consistent part quality throughout the production week.
When a Conveyor Deburring Cell Is the Right Investment
Investing in automated surface finishing is a significant strategic decision for any fabrication shop. Determining whether a conveyor deburring cell is the right fit requires analyzing financial data, understanding necessary custom features, and applying a structured selection methodology.
Evaluate Total Cost of Ownership
Evaluating the Total Cost of Ownership (TCO) is paramount. The initial capital expenditure for an industrial-grade conveyor deburring cell generally ranges from $50,000 to over $250,000, depending on the working width and number of finishing heads. However, TCO must also factor in electrical consumption—typically driven by main motors ranging from 20kW to 60kW—as well as the ongoing costs of abrasive belts, brushes, and dust collection filters over a projected 5 to 10-year lifecycle.
Ask the Right Customization and Sourcing Questions
Buyers must ask the right customization and sourcing questions to ensure the machine fits their specific part mix. If a facility processes small components (e.g., smaller than 50mm x 50mm), they must inquire about magnetic conveyor tracks or vacuum hold-down systems to prevent parts from flying off the belt. Additionally, questions regarding the availability of automated return conveyors or integrated part-flipping mechanisms are crucial for shops looking to minimize operator footprint and achieve true single-operator processing for double-sided finishing.
Use a Final Selection Framework
A final selection framework should culminate in a strict Return on Investment (ROI) calculation. Most high-volume fabricators target a payback period of 12 to 18 months. This rapid ROI is typically achieved by reallocating manual grinding labor to higher-value tasks, virtually eliminating scrap caused by inconsistent manual finishing, and increasing the overall speed of part delivery to downstream assembly. When these metrics align, the integration of a conveyor deburring cell transitions from a capital expense to a critical driver of manufacturing profitability.
Key Takeaways
- Use a conveyor deburring cell when production requires continuous one-piece flow from cutting to finishing without building excess work-in-progress inventory.
- Match the working width to your parts, with common conveyor deburring systems ranging from 600mm for compact cells to 1500mm or more for large sheet formats.
- Set conveyor feed rates between 1.0 and 10.0 meters per minute based on burr size, material condition, and the required edge rounding result.
- Choose automated conveyor deburring over manual grinding when 5-20 parts per hour is no longer enough to meet throughput or consistency targets.
- Consider conveyor deburring for applications needing repeatable edge radii up to 2.0mm across multiple part edges in a single continuous pass.
Frequently Asked Questions
What is a conveyor deburring cell?
A conveyor deburring cell is an automated finishing system that moves parts continuously through abrasive belts, brushes, or discs to remove burrs, round edges, and prepare metal components for downstream processes.
What parts are best suited for conveyor deburring?
It is best suited for flat or semi-flat sheet metal, machined plates, laser-cut parts, and extrusions, especially where high volume, repeatability, and safe edge conditions are required.
How fast can a linear conveyor deburring cell run?
Typical conveyor feed rates range from 1.0 to 10.0 meters per minute, depending on burr severity, material type, abrasive setup, and the required edge radius or surface finish.
How does conveyor deburring compare with manual grinding?
Manual grinding may process only 5-20 parts per hour and depends heavily on operator skill, while conveyor deburring supports continuous throughput with more consistent edge quality and lower labor dependency.
Can conveyor deburring handle large sheet metal parts?
Yes. Standard working widths often range from 600mm to 1500mm or more, making conveyor systems suitable for larger flat components that cannot be efficiently processed in batch tumbling equipment.