


High-volume finishing of circular parts is rarely limited by polishing quality alone; it is often constrained by cycle time, consistency, and tolerance control. Rotary disc polishing addresses that challenge by using centrifugal force to create intense, repeatable media contact across outer diameters, inner diameters, and flat faces. For manufacturers producing washers, gears, bearing rings, shims, or coin blanks, the process can reduce bottlenecks while improving surface uniformity. This article explains how the technology works, which parts benefit most, what specifications to evaluate, and why careful control of speed, media, compound, and gap settings is essential for reliable production results.
Why Rotary Disc Polishing Matters for High-Volume Circular Parts
Mass finishing of circular components demands rigorous control over material removal rates and surface uniformity. In modern manufacturing, rotary disc polishing—also widely known as centrifugal disc finishing, as the terms are essentially synonymous—provides an aggressive yet highly controllable mechanical action tailored for high-volume production environments.
Unlike traditional tumbling, this method processes thousands of parts simultaneously while maintaining strict dimensional tolerances. For manufacturers dealing with large volumes of round components, integrating this technology can be a highly effective strategy for reducing production bottlenecks.
What Rotary Disc Polishing Is
At its core, the technology relies on a stationary cylindrical work bowl featuring a rotating base, or spinner disc. As the disc rotates at speeds between 60 and 300 RPM, centrifugal forces propel the abrasive media and workpieces outward against the stationary polyurethane-lined wall.
This dynamic creates a continuous, high-energy toroidal (doughnut-shaped) rolling action. The resulting kinetic energy exerts up to 20 times the force of gravity (20G) on the parts, significantly accelerating the deburring, radiusing, and polishing phases compared to standard gravitational tumbling.
Which Circular Parts Benefit Most
Circular and symmetrical parts—such as stamped washers, gears, bearing rings, coin blanks, and precision shims—are the primary beneficiaries of this kinetic profile. While robust parts easily withstand aggressive media impingement without suffering geometric distortion, thin or soft circular components—such as aluminum or copper shims—require careful process tuning to prevent deformation under high G-forces.
Rather than being constrained by arbitrary part diameters, suitability is primarily governed by the relationship between bowl volume, media size, and the machine's gap settings. When properly configured, the homogeneous flow ensures that outer diameters, inner diameters, and flat faces receive uniform abrasion, rapidly reducing surface roughness (Ra) values while maintaining the tight dimensional tolerances required for aerospace, automotive, and medical applications.
How Rotary Disc Polishing Improves Throughput
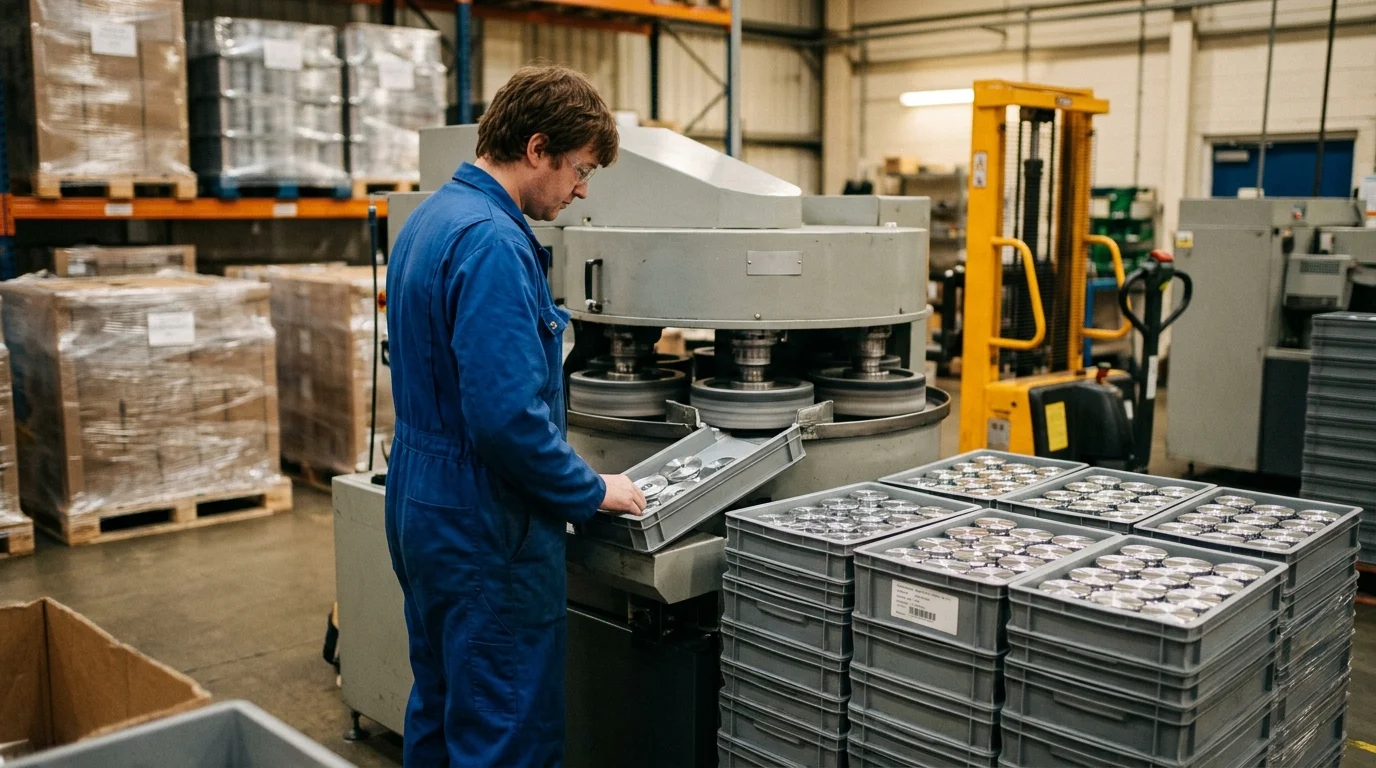
Throughput in mass finishing relies on maximizing the physical force transferred to the workpiece without compromising surface integrity. Rotary disc systems achieve rapid cycle times by continuously forcing the media-compound matrix against the parts at high velocities, effectively multiplying the cutting action per minute of operation.
Key Machine Specifications
Industrial rotary disc machines are defined by their motor power, bowl volume, and precision gap controls. High-capacity units typically feature drive motors ranging from 5 kW to 22 kW, supporting bowl volumes between 20 and 120 liters.
A critical specification is the gap between the rotating disc and the stationary wall. To prevent thin circular parts or fine media from jamming and causing severe machine wear, this gap must be dynamically adjustable. While often maintained at fractions of a millimeter, exact gap widths vary widely by OEM and media size. Advanced systems utilize water-cooled gap rings to mitigate the thermal expansion caused by high-friction processing.
Media, Compound, and Geometry Factors
The interaction between the workpiece and the media is mediated by the compound, which provides lubricity, suspends particulate matter, and prevents part-on-part adhesion. For circular parts, selecting a media geometry that prevents lodging in inner diameters is paramount.
High-density ceramic media is favored for rapid deburring, while plastic or porcelain media is deployed for fine polishing. Compound dosing systems continuously inject solutions at OEM-specified rates, ensuring continuous flushing of the abrasive slurry and maintaining optimal cutting conditions without relying on guesswork.
Cycle Time and Quality Metrics
The aggressive nature of the toroidal flow can drastically reduce cycle times compared to conventional methods, though the exact time savings depend heavily on incoming burr size, starting surface finish, and media condition. A process that requires three hours in a standard tub vibrator can often be completed in a fraction of the time in a rotary disc machine. The table below presents purely illustrative example ranges for cycle times and surface finishes; published quality metrics, such as achieving an Ra reduction from 3.2 µm to 0.4 µm, are achievable within these compressed timeframes provided the prior process steps are properly controlled.
| Material | Application | Example Cycle Time Range (Mins) | Example Target Ra Range (µm) |
|---|---|---|---|
| Carbon Steel | Heavy Deburring | 20 - 35 | 0.8 - 1.2 |
| Stainless Steel | Pre-Plate Polishing | 15 - 25 | 0.2 - 0.4 |
| Brass / Copper | Deflashing & Burnishing | 10 - 15 | 0.1 - 0.3 |
| Titanium | Edge Radiusing | 30 - 45 | 0.4 - 0.6 |
Rotary Disc Polishing vs. Vibratory Finishing
While vibratory finishing remains the ubiquitous standard for general-purpose mass finishing, rotary disc technology occupies a specialized, high-performance niche. Understanding the mechanical and economic differences is essential for process engineers optimizing a production line.
Cost, Speed, and Finish Quality Comparison
The fundamental divergence between the two technologies lies in their energy generation and application. Vibratory bowls rely on eccentric weights to generate a low-amplitude, high-frequency scrubbing action, whereas rotary discs utilize centrifugal force for high-pressure impingement.
It is important to note the operational cost implications of this high-energy process. While cycle times are significantly faster, the intense 10G to 20G forces result in accelerated media consumption. This high media wear rate increases consumable costs and requires more frequent replenishment, a factor that must be carefully weighed against the productivity gains when calculating the total cost of ownership.
| Metric | Rotary Disc Polishing | Vibratory Finishing |
|---|---|---|
| Operating Force | 10G - 20G | 3G - 5G |
| Typical Cycle Time | 15 - 45 Minutes | 2 - 6 Hours |
| Media Wear Rate | High | Low |
| Equipment CapEx | Premium | Standard |
| Suitability for Fragile Parts | Low to Moderate | High |
When Rotary Disc Polishing Performs Better
Rotary disc polishing is often preferred when throughput velocity is the primary constraint. It performs exceptionally well for high-volume batches of flat, circular components that require heavy radiusing or rapid oxide removal.
Conversely, vibratory finishing is better suited for heavy, asymmetrical, or highly fragile components that might suffer impingement damage under high G-forces. The higher capital and consumable costs of rotary systems are rapidly amortized when processing millions of small circular parts annually, where reducing multi-hour cycles to a fraction of the time drastically cuts work-in-progress (WIP) inventory.
How to Implement Rotary Disc Polishing
Successful deployment of a rotary disc polishing system requires meticulous process engineering, from initial part loading to post-process handling. Integrating these machines into an existing line requires strict operational protocols.
Part Loading and Fixture Validation
Circular parts, particularly flat washers or shims, are prone to "nesting" or adhering to one another due to surface tension, which prevents uniform media contact. To counteract this, operators must validate the volumetric media-to-part ratio, which typically ranges from 3:1 to 5:1.
Instead of mixing different media sizes—which can cause size-classification issues, uneven finishing, and loading problems—operators should utilize OEM-approved anti-nesting media shapes (such as angle-cut cylinders) or specialized fixture solutions. Furthermore, operators must be cautious of part-on-part impingement damage in high-G flows; thin circular parts can easily deform from mutual impact even when anti-nesting media is used. Proper loading sequencing—introducing media and water first, followed by the gradual addition of parts—helps prevent initial impact damage at the bottom of the bowl.
Maintenance and Safety Requirements
High-energy processing subjects the machinery to severe abrasive wear. The hot-poured polyurethane lining requires routine inspection and must be recast when wear exceeds manufacturer-specified thresholds. The precision gap between the spinner and the bowl wall demands daily calibration to prevent damaging media jamming.
From a safety and environmental perspective, the acoustic output of rotary disc machines can exceed 85 decibels, depending on the equipment and media used. Implementing sound-dampening enclosures is standard practice to comply with regional occupational noise limits or general guidelines such as ISO 11202 for machinery noise emission. Additionally, facilities must implement standard machine guarding, protect operators from thermal exposure to hot abrasive slurries, and establish compliant waste disposal protocols for spent compound and media effluent.
Upstream and Downstream Process Alignment
Rotary disc polishing cannot operate in a vacuum; it must be tightly integrated with adjacent manufacturing steps. Upstream processes like stamping or fineblanking should be optimized to limit primary burr heights to less than 0.5 mm, as excessive burrs will rapidly degrade the polishing media.
Downstream, the high throughput of the disc machine requires automated separation systems. Following separation, parts must immediately enter centrifugal dryers or continuous mesh-belt drying ovens treated with corrosion inhibitors to prevent flash rusting of freshly exposed metal surfaces.
How to Select a Rotary Disc Polishing Machine
Procuring the right rotary disc polishing machine involves balancing initial capital expenditure against long-term operational efficiencies, automation needs, and precise application requirements. It is also crucial to recognize that rotary disc polishing is not universally optimal for all circular parts; small lot sizes, highly fragile features, or complex geometries may still favor vibratory or drag finishing.
Cost Drivers and Supplier Capabilities
Capital costs for centrifugal disc systems are driven by bowl capacity, motor drive technology, and the degree of automation. Depending heavily on the supplier and region, entry-level, manual-tilt machines require a higher initial investment than standard vibratory tubs, with costs scaling significantly for fully automated tandem systems featuring programmable logic controllers (PLCs), hydraulic tilt mechanisms, and integrated magnetic separators.
Supplier capabilities should be evaluated based on their ability to provide custom polyurethane durometers, reliable gap-adjustment mechanisms, and responsive technical support for consumable replenishment. A supplier's ability to run sample processing trials before purchase is a critical indicator of their process expertise.
Capacity and Application Fit
Selecting the correct capacity requires calculating the total daily volume of parts and dividing it by the expected batches per hour. For instance, processing 20,000 bearing rings per day with a media-to-part ratio of 4:1 and a 20-minute cycle time will dictate a specific bowl volume, often requiring a 60-liter machine running continuously across shifts.
Application fit also dictates the choice of gap design. Ultra-thin circular parts under 1 mm in thickness require machines with zero-gap designs or highly sophisticated ceramic gap rings to ensure seamless, uninterrupted processing without material loss or mechanical binding.
Key Takeaways
- Use rotary disc polishing for high-volume circular parts when fast deburring, radiusing, and surface uniformity are required.
- Select machine capacity based on bowl volume, motor power, media size, and part geometry rather than part diameter alone.
- Maintain a precisely adjustable disc-to-wall gap to prevent jamming, reduce machine wear, and protect thin components.
- Tune speed, media, compound, and cycle time carefully when processing soft metals such as aluminum or copper.
- Expect much faster finishing than conventional tumbling because rotary disc systems can generate up to 20G of processing force.
Frequently Asked Questions
What is rotary disc polishing best used for?
Rotary disc polishing is best suited for high-volume deburring, radiusing, and surface finishing of circular or symmetrical parts such as washers, gears, bearing rings, coin blanks, and precision shims.
How fast does a rotary disc polishing machine operate?
Typical rotary disc systems run at about 60 to 300 RPM, generating a high-energy rolling action that can apply up to 20G of force to parts and media.
Why is rotary disc polishing faster than traditional tumbling?
It uses centrifugal force to intensify media contact, multiplying cutting action per minute. This allows thousands of parts to be processed simultaneously while maintaining surface uniformity and dimensional control.
Can thin aluminum or copper parts be polished safely?
Yes, but they require careful tuning of speed, media size, compound, and gap settings. Excessive force can deform thin or soft circular parts if the process is too aggressive.
What machine specifications matter most?
Key specifications include bowl volume, motor power, adjustable disc-to-wall gap, media compatibility, and cooling design. Industrial systems often use 5 kW to 22 kW motors and 20 to 120 liter bowls.