


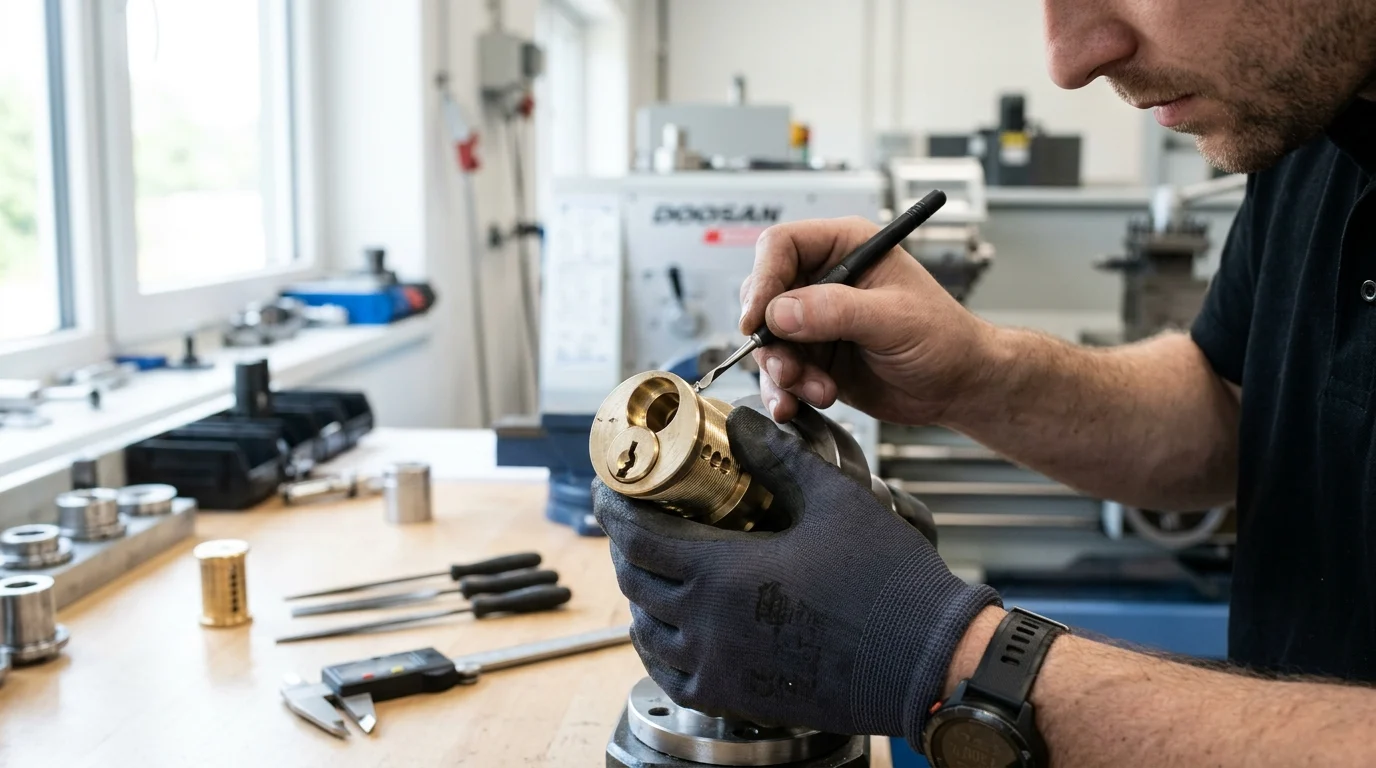
Door lock manufacturing is shifting from simple mechanical hardware to precision electromechanical security assemblies, and that shift is raising the stakes for every edge, hole, and latch surface. As smart locks incorporate micro-motors, optical sensors, gear trains, and tight-tolerance moving parts, even a microscopic burr can compromise performance or trigger costly defects. For manufacturers producing hundreds of thousands of units annually, manual finishing is no longer enough to meet modern quality expectations. This article examines why automated deburring is becoming essential in the door lock industry, which components need the most attention, and how defined edge standards help improve reliability, consistency, and production efficiency.
Why Door Lock Deburring Demand Is Rising
The global transition toward electromechanical access control has fundamentally altered the manufacturing paradigms for door lock hardware. As mechanical pin-and-tumbler systems merge with digital actuators, demand for door lock deburring has surged, driven by the absolute necessity for precision. Automated deburring is no longer a secondary finishing step; it is a manufacturing gateway that dictates the functional viability of the final assembly.
Higher production volumes and quality expectations
The commercial and residential security sectors are experiencing unprecedented scale, with tier-one hardware manufacturers routinely exceeding typical production volumes of 500,000 to 1 million units annually per facility. At this scale, legacy manual finishing creates severe production bottlenecks. Furthermore, acceptable defect rates have plummeted. Industry-leading OEMs now often target defect rates below 50 PPM (parts per million)—an estimated threshold that is virtually unattainable when relying on the subjective consistency of manual hand-tool deburring.
Smart lock complexity and tighter tolerances
Smart locks integrate micro-motors, optical sensors, and intricate gear trains directly alongside traditional heavy-duty latches. This convergence requires dimensional tolerances as tight as +/- 0.015 mm on internal moving components. A single microscopic burr measuring just 0.02 mm can dislodge during operation, jamming a motorized deadbolt or obstructing an optical encoder. To comply with international quality protocols, manufacturers must eliminate these micro-burrs completely to ensure the long-term reliability of battery-powered lock mechanisms.
Components with the highest deburring needs
While external escutcheons require purely cosmetic finishing, internal moving components demand the highest degree of functional, precision deburring. Brass cylinders, zinc die-cast gear housings, stainless steel 304 strike plates, and hardened steel locking pins are the primary candidates. Specifically, the shear edges of stamped steel latches and the internal intersecting cross-holes of CNC-machined brass plug bodies represent the most sensitive geometries where burr removal directly correlates to the lock's tactile smoothness and anti-pick resistance.
What Automated Deburring Means for Lock Components
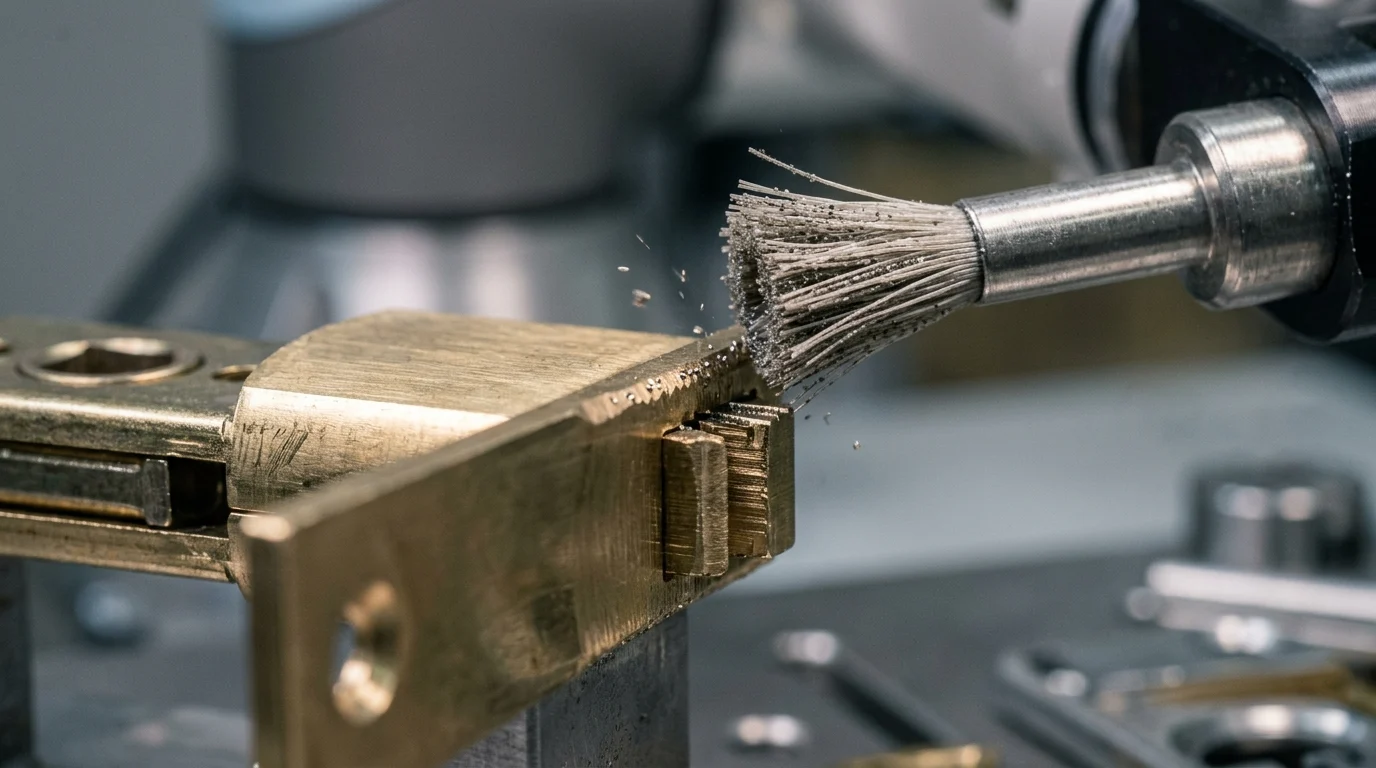
Transitioning to automated deburring requires a fundamental shift from qualitative visual inspections to repeatable, quantifiable edge profiling. For door lock components, defining what constitutes a finished edge is the first step in engineering an automated solution.
Defining acceptable burrs and edge breaks
In precision hardware manufacturing, an acceptable edge state must be explicitly defined on engineering drawings. Standard specifications often require positive edge breaks ranging from 0.05 mm to 0.20 mm, ensuring the removal of sharp anomalies without altering the component's base geometry. Automated systems are programmed to achieve these specific edge radii consistently, eliminating the ambiguity of "break all sharp edges" notes that historically led to over-machining.
Common burr sources in stamping, casting, and CNC machining
Different manufacturing processes generate distinct burr morphologies. High-speed stamping of strike plates typically produces breakaway burrs and rollover edges that can exceed 0.1 mm in height. Zinc and aluminum die-casting processes, widely used for lock chassis and handles, leave parting line flash that often ranges from 0.05 mm to 0.15 mm depending on mold wear. Meanwhile, CNC machining of brass lock cylinders generates complex, tenacious rollover burrs at the intersections of drilled pin chambers, requiring targeted mechanical or abrasive energy for removal.
Quality risks from inconsistent manual deburring
Relying on manual labor for deburring introduces severe quality risks, primarily due to operator fatigue and applied force variations. Inconsistent manual chamfering can inadvertently widen pin chambers, causing excessive key play or compromising the lock's shear line. Facilities relying on manual finishing can see scrap rates escalate to an estimated 3–5% in some scenarios solely due to over-chamfering or missed internal burrs. Automated deburring mitigates these risks by applying uniform mechanical profiles to every component.
How to Compare Automated Deburring Technologies
Selecting the appropriate automated deburring technology requires a systematic analysis of mechanical energy transfer, media type, and the specific geometries of the lock components. No single technology acts as a panacea for all hardware finishing requirements.
Key process comparison criteria
When comparing automated solutions, operations managers and manufacturing engineers must evaluate cycle time, consumable media costs, capital expenditure (CapEx), and surface roughness (Ra) improvements. A high-volume stamping line may prioritize rapid cycle times (e.g., under 15 seconds per part) and continuous throughput, while a machining cell producing high-security brass cylinders may prioritize internal edge precision and target an Ra of < 0.4 µm on sliding surfaces, justifying a longer cycle time. Bridging these technical specifications with operational goals ensures the chosen system aligns with broader business objectives.
Robotic brushing, vibratory finishing, and abrasive flow options
Robotic brushing utilizes multi-axis articulating arms equipped with abrasive nylon or wire wheels, offering programmable, directional force control ideal for complex exterior geometries like lock handles. Vibratory finishing is a bulk mass-finishing process where parts are submerged in ceramic or plastic media, highly cost-effective for large batches of small components like pins and tumblers. Abrasive flow machining (AFM) extrudes a viscoelastic abrasive polymer through internal cavities, making it the premier choice for polishing the intersecting cross-holes of complex lock cylinders.
Matching technology to part geometry and material
Matching the technology to the component is essential for optimizing both throughput and edge quality. It is also important to note that high-security lock components often require multi-stage (hybrid) finishing workflows. Rather than relying on a single automated step, manufacturers may use sequential deburring methods—such as vibratory finishing followed by targeted robotic brushing—to achieve the necessary edge quality. The table below outlines typical alignments and key limitations in modern lock manufacturing.
Note: The Ra values and cycle times presented are representative ranges; actual outcomes depend heavily on media type, part geometry, and specific equipment models.
| Technology | Optimal Lock Component | Compatible Materials | Target Ra (µm) | Key Limitations |
|---|---|---|---|---|
| Robotic Brushing | Exterior Handles, Escutcheons | Brass, Zinc, Stainless Steel | 0.4 - 0.8 | High initial CapEx; struggles to reach deep internal cross-holes. |
| Vibratory Finishing | Tumbler Pins, Small Latches | Brass, Hardened Steel | 0.2 - 0.6 | Rounds all edges uniformly; cannot target specific internal burrs. |
| Abrasive Flow (AFM) | Cylinder Plugs, Cross-holes | Brass, Nickel Silver | < 0.2 | Slower cycle times (45–90s); higher consumable media costs. |
| Centrifugal Disc | Stamped Strike Plates | Steel, Stainless Steel 304 | 0.5 - 1.0 | Part-on-part impingement risk for delicate or cosmetic components. |
How to Build a Stable Door Lock Deburring Process
Implementing automated deburring hardware is only part of the solution; establishing a stable, repeatable process requires strict control over upstream variables and rigorous inspection protocols.
Creating a burr map and part classification system
A robust automated process begins with a comprehensive burr map. This involves classifying burrs by root thickness and location. For example, Class 1 micro-burrs (< 0.05 mm root thickness) can typically be removed via light vibratory finishing, while Class 2 macro-burrs (0.05 mm to 0.15 mm) generated by worn stamping dies require aggressive robotic brushing or belt sanding. Systematizing parts by these classifications allows engineers to standardize media selection and robotic tool paths.
Managing cycle time, changeover, and upstream process variation
High-volume lock assembly lines operate on aggressive takt times, frequently demanding a finished component every 10 to 15 seconds. Automated deburring cells must not only meet this cycle time but also accommodate upstream variations. As cutting tools wear or casting dies degrade, burr sizes increase. Modern robotic deburring cells manage this through active compliance devices—spindles equipped with adaptive force control that can dynamically adjust applied pressure, with a sensitivity often reaching +/- 2 Newtons on industry-standard equipment, ensuring consistent edge breaks regardless of incoming burr variance.
Inspection methods for consistent edge quality
To validate the automated process, lock manufacturers must deploy advanced metrology. Tactile profilometers are used to verify that surface roughness remains below the required 0.8 µm threshold on internal sliding surfaces. For edge break verification, non-contact optical comparators and 3D laser scanning microscopes provide high-resolution cross-sectional data, confirming that the automated system is consistently achieving the specified 0.05 mm to 0.20 mm edge radius without inducing secondary burrs.
How to Justify Investment and Select Suppliers
Capital expenditure in automated deburring systems is traditionally justified through direct labor offset, but in the highly competitive door lock industry, financial decision-makers and CFOs must ensure the ROI calculation encompasses quality yields, warranty reductions, and compliance factors.
Cost, quality, labor, warranty, safety, and compliance factors
As manufacturing labor rates continue to rise globally, manual deburring becomes increasingly cost-prohibitive in many regions. A hypothetical cost-per-part analysis for a high-wage market might reveal that manual deburring costs approximately $1.20 per complex lock cylinder, whereas an optimized robotic cell could reduce this to an estimated $0.22 per part. However, a balanced financial analysis must also account for hidden operational costs. These include ongoing abrasive media replenishment, end-of-arm tooling (EOAT) replacement, programming labor for new part introductions, and recalibration downtime. Beyond direct labor and operating expenses, automated systems drastically reduce repetitive strain injury (RSI) claims, lower environmental dust exposure, and ensure compliance with stringent occupational safety mandates.
Supplier capabilities that reduce launch risk
Selecting the right integration partner mitigates launch risks. Manufacturers should mandate comprehensive Proof of Concept (PoC) testing using actual production parts before finalizing equipment purchases. Essential supplier capabilities include local integration support, remote diagnostics, and a target Mean Time Between Failures (MTBF) exceeding 5,000 hours. Suppliers who offer interchangeable end-of-arm tooling (EOAT) also provide the flexibility needed to adapt to future lock designs.
ROI metrics for automated deburring projects
The financial justification for automated deburring is highly compelling when all operational metrics are quantified, though it is important to note that these assumptions primarily apply to high-volume OEMs. High-mix, low-volume, or custom lock manufacturers may not achieve a viable ROI with full automation, and manual methods often remain the most appropriate choice for prototyping and short production runs. For tier-one hardware facilities, however, achieving an estimated payback period of 12 to 18 months is a common target.
| Operational Metric | Hypothetical Manual Baseline | Automated System Estimate | Variance / Financial Impact |
|---|---|---|---|
| Unit Finishing Cost | ~$1.20 / part | ~$0.22 / part | Estimated 81% reduction in direct costs |
| Scrap / Rework Rate | Up to 3.5% | < 0.2% | Recovers thousands of parts annually |
| Throughput Variance | High (operator dependent) | Zero (highly repeatable) | Enables predictable downstream assembly |
| Changeover Time | 15 - 20 minutes | < 2 minutes (recipe driven) | 90% reduction in downtime |
Ultimately, transitioning to automated deburring is no longer just a tactical manufacturing upgrade; it is a strategic necessity for high-volume modern lock producers. By combining the right technology with rigorous process controls, manufacturers can eliminate the inconsistencies of manual labor, meet the exacting tolerances of electromechanical hardware, and secure a competitive advantage in a rapidly evolving security market.
Further reading:
Key Takeaways
- Define edge-break requirements on engineering drawings, such as 0.05 mm to 0.20 mm, before implementing automated deburring.
- Prioritize automated deburring for internal moving parts because burrs near 0.02 mm can disrupt smart lock motors, sensors, and gear trains.
- Use automated systems when production approaches 500,000 to 1 million units per facility, as manual finishing can become a major bottleneck.
- Target repeatable, measurable edge profiles to support defect-rate goals below 50 PPM in high-volume door lock manufacturing.
- Match the deburring process to the burr source, since stamping, CNC machining, and die casting create different burr types and edge conditions.
Frequently Asked Questions
Why is deburring becoming more important in door lock manufacturing?
Smart locks combine mechanical parts with motors, sensors, and gear trains, making burr-free edges critical for smooth movement, reliability, and low defect rates.
What defect rate do leading door lock OEMs typically target?
Many leading manufacturers target defect rates below 50 PPM, which is difficult to achieve with inconsistent manual deburring at high production volumes.
Which door lock components need the most precise deburring?
Brass cylinders, CNC-machined plug bodies, stamped latches, stainless steel strike plates, zinc die-cast housings, and hardened locking pins usually require the highest deburring control.
How small can a burr be before it causes lock failures?
A burr as small as 0.02 mm can interfere with smart lock mechanisms by jamming a motorized deadbolt or obstructing an optical encoder.
What edge break is commonly specified for precision lock hardware?
Engineering drawings often specify positive edge breaks from 0.05 mm to 0.20 mm to remove sharp burrs without changing the component’s functional geometry.